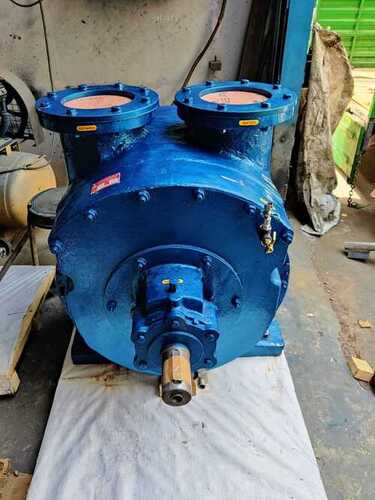
About 65 HP Single Stage Water Ring Vacuum Pump
The 65 HP Single Stage Water Ring Vacuum Pump is a high-performance industrial vacuum solution designed for efficient and reliable operation in demanding applications. It uses a rotating impeller and liquid ring mechanism to generate vacuum, ensuring smooth performance and consistent suction. Manufactured with robust materials and advanced engineering, this pump offers excellent durability, low maintenance, and dependable operation. It is widely used in chemical processing, pharmaceutical industries, paper mills, food processing, power plants, and industrial manufacturing units. Its efficient design, continuous-duty capability, and reliable vacuum generation make it suitable for various industrial vacuum requirements.
Versatile Industrial ApplicationsThis 65 HP water ring vacuum pump is engineered for versatility, supporting a wide array of industries including oil wells, food processing, automobile manufacturing, cosmetics, paper printing, and maritime applications. Its robust structure ensures consistent performance even in challenging environments, delivering optimal results and reliability.
Durable Cast Iron ConstructionFeaturing cast iron material, the pump offers superior durability and resistance to wear, making it suitable for continuous industrial usage. Its sturdy build attenuates damage from corrosive elements and heavy duty operations, allowing for lasting functionality and minimal maintenance over time.
FAQ's of 65 HP Single Stage Water Ring Vacuum Pump:
Q: How does the 65 HP Single Stage Water Ring Vacuum Pump function in industrial environments?
A: This vacuum pump operates using water ring theory, generating a vacuum by creating a liquid seal in a single stage chamber. It efficiently removes gases and vapors from industrial processes, making it suitable for continuous operation in applications such as oil wells, cryogenic systems, sewage treatment, and food manufacturing.
Q: What are the key benefits of using this pump in industries like oil well and food processing?
A: The pump offers reliable performance, efficient air removal, and versatile operation across multiple sectors. Its durable cast iron body ensures longevity, while the 65 HP power delivers robust suction capacity. This results in improved productivity, reduced downtime, and consistent process stability.
Q: When should this water ring vacuum pump be selected over other types of pumps?
A: It is recommended when processes require efficient vacuum generation, especially in applications involving handling gases, vapors, or liquids in industrial settings. Its single-stage design is optimal for operations needing moderate vacuum levels with high reliability.
Q: Where is the 65 HP Single Stage Water Ring Vacuum Pump commonly installed?
A: This pump is installed in various facilities such as maritime ports, sewage treatment plants, metering stations, automotive factories, cosmetic manufacturing units, paper printing facilities, and food processing plants, primarily where reliable vacuum and gas removal are essential.
Q: What is the process for exporting and supplying this pump from India?
A: Manufactured in India, the pump is supplied by recognized exporters, manufacturers, and suppliers. Orders involve quality inspection, customization as per industry requirement, secure packaging, and safe delivery to international and domestic clients.
Q: How is this vacuum pump used in metering and cryogenic operations?
A: In metering applications, the pump facilitates accurate measurement of fluids by maintaining consistent vacuum conditions. For cryogenic processes, it helps remove air and moisture for efficient cooling and liquefaction of gases, ensuring equipment safety and operation precision.





 Send Inquiry


 Send Inquiry
